Industrial gases like oxygen and nitrogen quietly power some of the world’s most essential industries — steel, chemical processing, pharmaceuticals, healthcare, and more. Behind these gases lies an impressive mix of engineering, precision, and innovation. One company that has refined this technology over decades is Sanghi Organization, known for its efficient and reliable air separation systems.
In this article, we explore how modern oxygen/nitrogen plants work, what makes them efficient, and the manufacturing excellence behind them.
What Makes Modern Oxygen/Nitrogen Plants So Efficient?
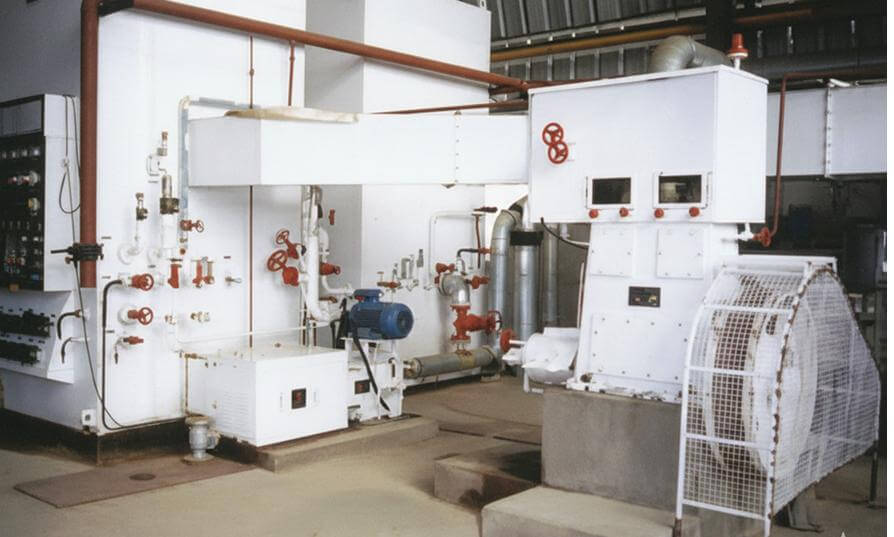
Today’s air separation units are designed not only to produce gases with extremely high purity but to do so safely, economically, and with minimal maintenance. The Sanghi-Org. Oxygen Plant, for example, is built as a medium-pressure system that significantly reduces power consumption through optimized expansion engines and smart pressure management.
At the heart of the plant is a molecular sieve battery assembly, a technology that removes moisture and carbon dioxide from atmospheric air before it enters the cryogenic process. This not only improves gas purity but also enhances the life and efficiency of the plant.
These plants are engineered for flexibility too — capable of producing oxygen and nitrogen simultaneously, and even compressing liquid oxygen to fill cylinders directly.
How an Oxygen Plant Works: Step-by-Step
The production of oxygen begins with something incredibly simple: atmospheric air. But what happens next is a fascinating series of transformations involving pressure, temperature, and phase change.
1. Air Compression & Purification
Air is sucked in through a multi-stage compressor, passed through filters, and compressed. At each stage, intermediate coolers and water separators remove heat and moisture. After compression, the air passes through:
2.Heat Exchange & Cooling
The dry, clean air then enters a heat exchanger where it is cooled by outgoing waste nitrogen and the product oxygen stream.
3.Expansion & Liquefaction
Part of the cold air goes through an expansion machine, cooling further until portions of it liquefy. This ultra-cold air feeds into the lower pressure column of the distillation unit.
4.Fractional Distillation
Here, oxygen and nitrogen separate naturally due to their different boiling points:
5.Final Oxygen Extraction
The oxygen vapor undergoes final heat exchange steps, is filtered, and sent to the filling manifold via a liquid pump.
The result? Oxygen purities up to 99.5% and nitrogen purities above 99%, depending on plant configuration.
Standard Production Capacities
Sanghi offers a full range of capacities — from small 40 cu.m/hr units to massive 1000 cu.m/hr systems. Depending on plant size, oxygen output can reach 99.5% purity, and nitrogen can exceed 99.9%.
These performance numbers are based on ambient conditions and strict impurity allowances such as 300 ppm CO₂.
Operational Excellence: What Sets These Plants Apart
Precision Manufacturing: Built for Global Performance
Behind every air separation plant lies rigorous engineering and manufacturing. Sanghi’s facilities follow international standards and strict quality norms. Every plant is tested before shipment, ensuring fast startup and reliable operation on-site.
Key manufacturing strengths include:
Their plants have been installed across steel mills, chemical factories, pharmaceutical units, fiber optic manufacturing, and more — proving their versatility and trustworthiness.
Where Industrial Gas Technology Is Headed
With rising global demand for medical oxygen, cleaner industrial processes, and energy-efficient systems, modern oxygen/nitrogen plants are more essential than ever. Advances in cryogenic distillation, automation, and purification promise even higher efficiencies and lower operating costs in the future.
Companies adopting such plants gain:
As industries continue to evolve, the backbone technologies — separation, purification, and liquefaction — remain as relevant as ever.
Final Thoughts
The world of oxygen and nitrogen generation is a brilliant example of engineering mastery. From compressing simple air to producing high-purity gases, the process is both elegant and powerful.
If your organization depends on industrial gases, understanding the technology behind them — and choosing a reliable manufacturer — can dramatically improve your operational efficiency.